Pack King Machinery

-
-
-
-
Blog

Product Category
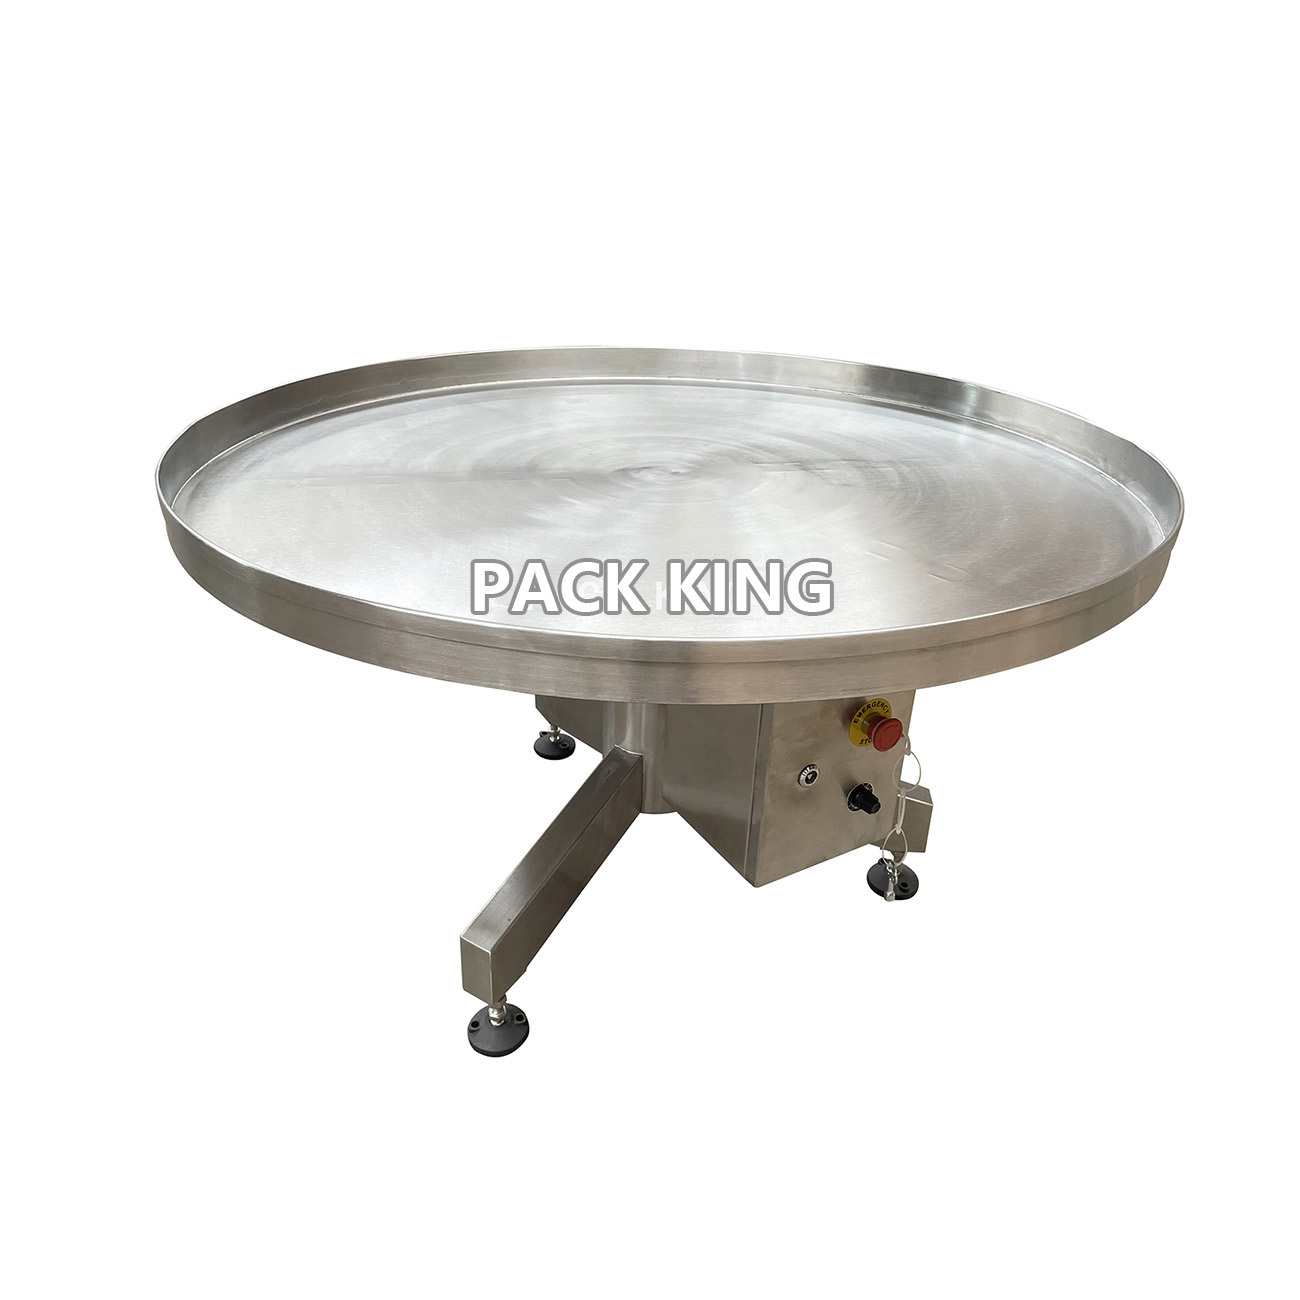
Function and Application: Flat surface rotary table collects food products packaged by the packaging machine by rotating, automatically ending the packaging process. The flat disc edge turns outward to prevent the packaged products from falling due to excessive accumulation.
MORE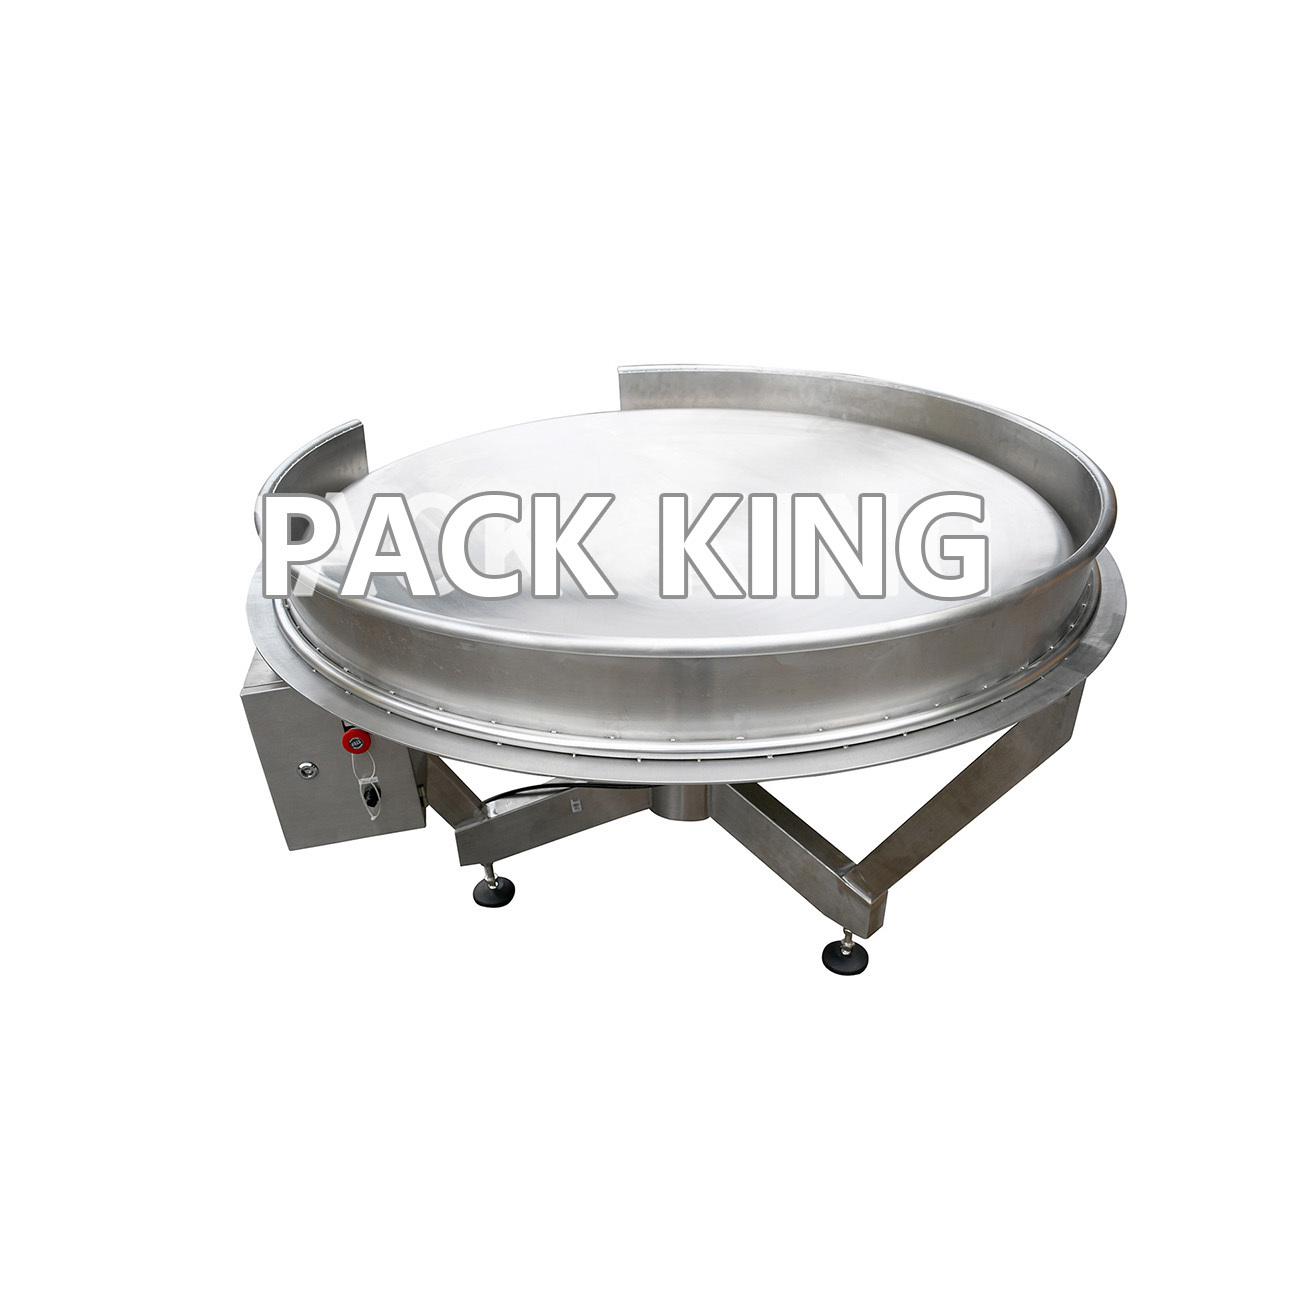
Flat surface rotary table with guardrail
Function and application: Finished products are mainly packaged by packaging machines and then transported to Flat surface rotary table with guardrail for packaging. The edge guard is suitable for smaller finished products to prevent materials from falling.
MORE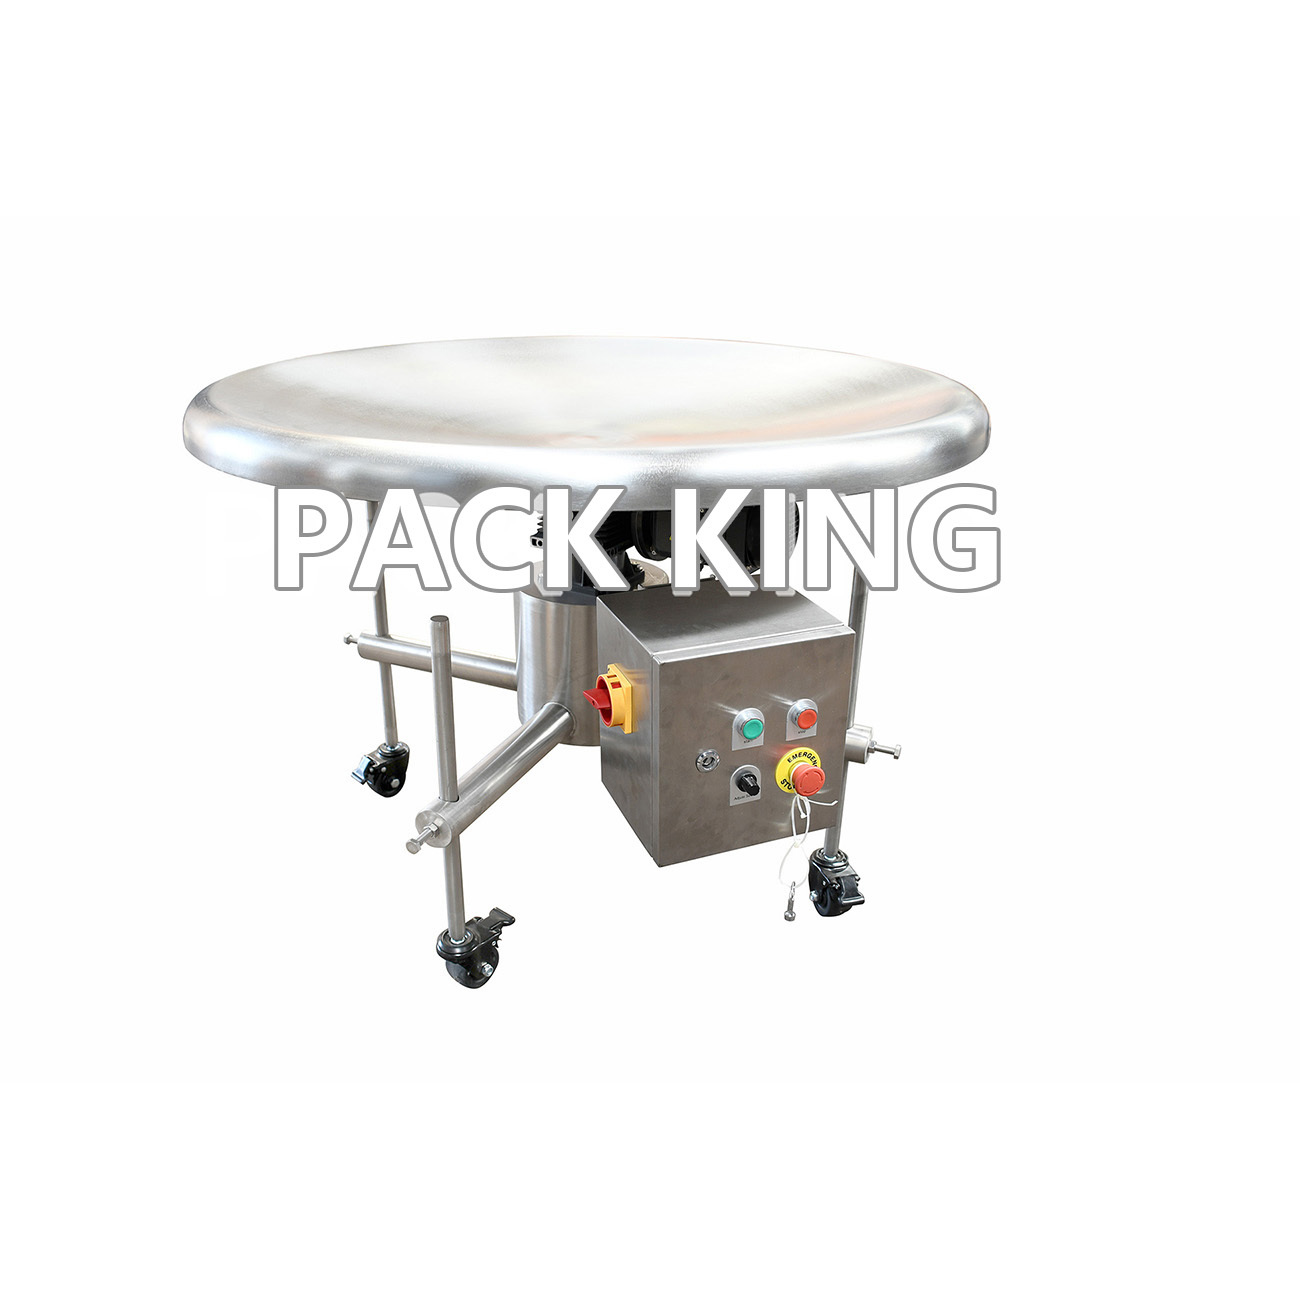
Flat rotary table with movable bracket
Function and application: The removable bracket design, equipped with silent universal wheels and a brake mechanism, easily adapts to different production line layouts, flexibly adjusting the spacing between devices according to the packaging machine's output position. It also remains firmly fixed during operation, ensuring the stability of the disc during rotation. Whether it's a tight workshop space or a production plan that requires frequent adjustments, it can quickly respond, eliminating the tedious steps of traditional fixed installation and significantly improving site utilization.
MORE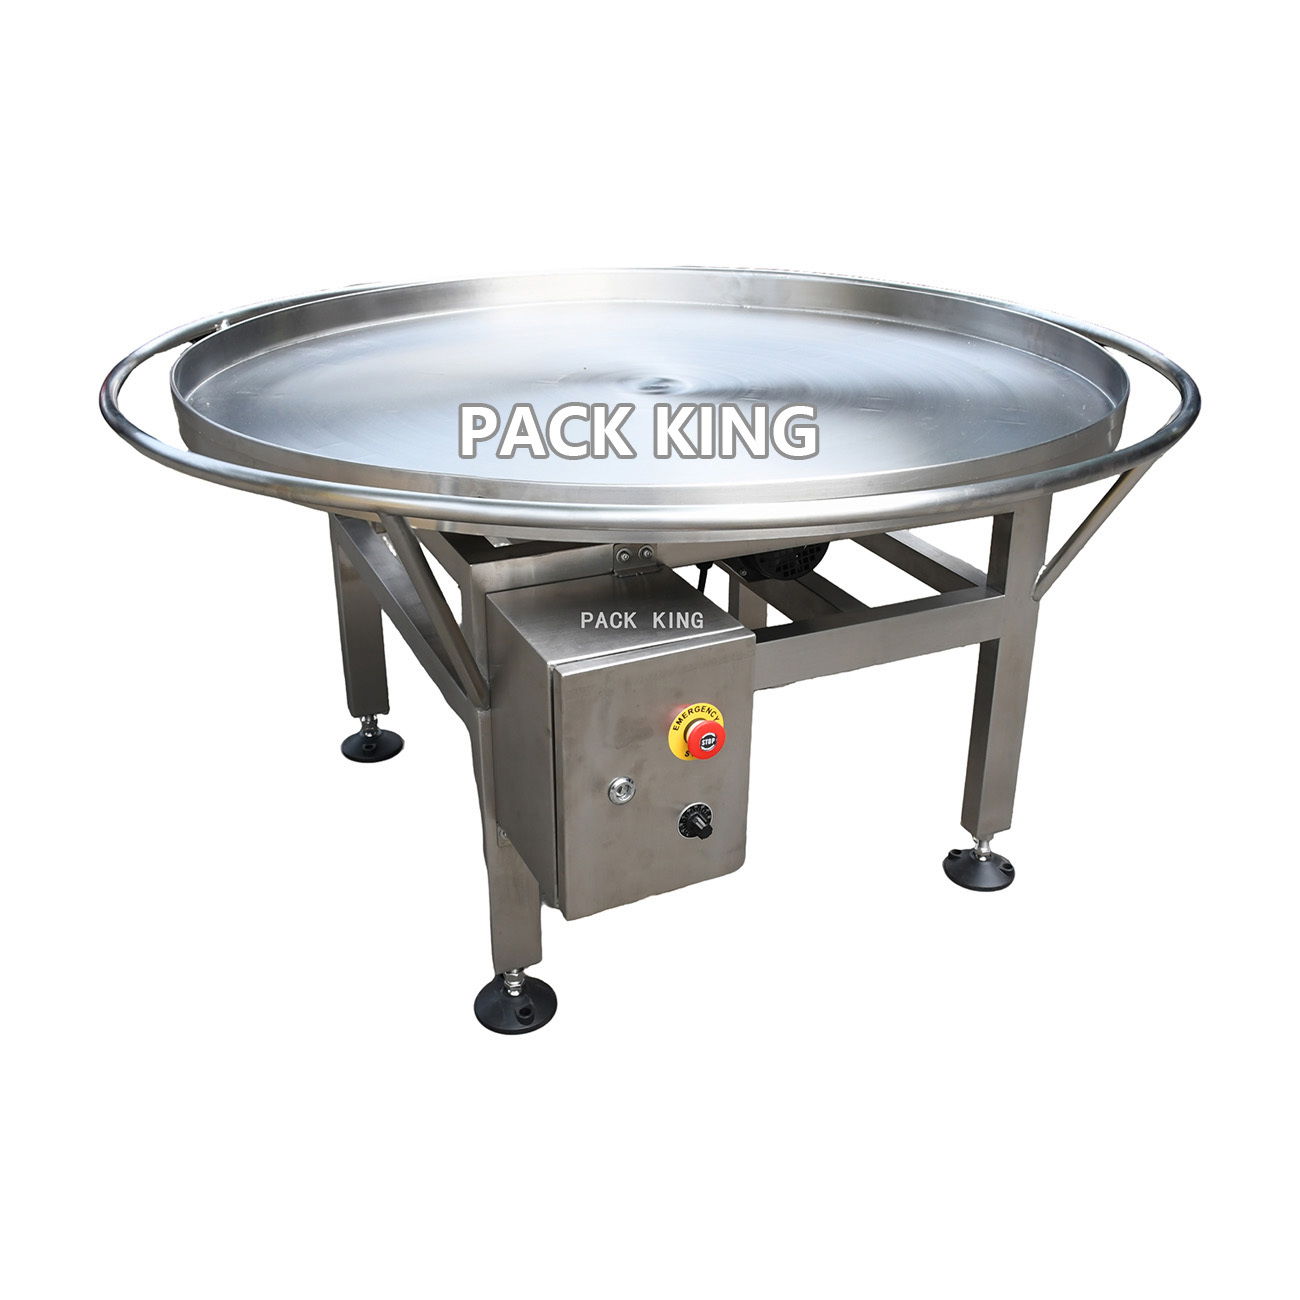
Flat rotary table with external guide rods
Function and application: After the packaging machine completes packaging of finished products, the materials are smoothly transported to the disc food processor via the conveyor system. The specially designed outer guide rod structure on its edge acts as a precise protective barrier, closely following the food's conveying trajectory. Guided by the guide rod, the finished products maintain an orderly posture, fundamentally preventing the materials from falling or bumping during transportation and packaging.
MORE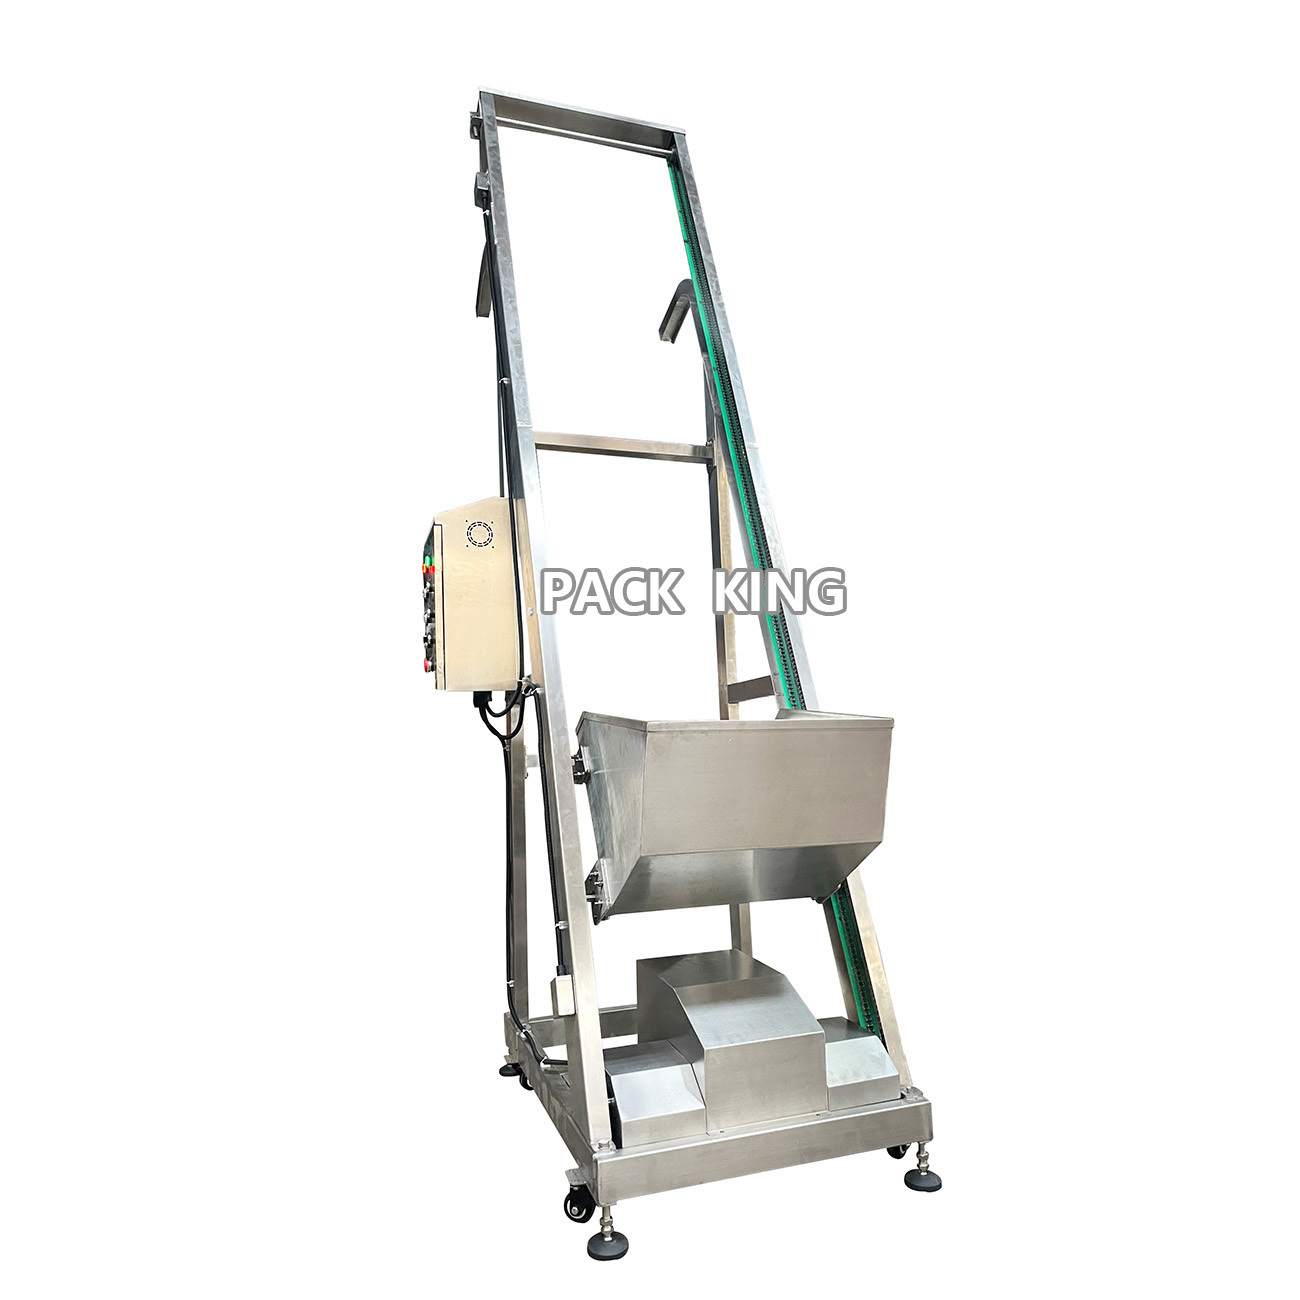
Single bucket elevator is a continuous conveying equipment used for vertically or steeply inclined transportation of bulk materials. Its core function is to achieve material lifting and transportation through the cyclic operation of individual buckets, widely applied in industries such as chemical, grain, snacks,dried fruits and meats processing. Inclined single-bucket elevator: A versatile workhorse for bulk material handling. Designed to lift granular/powdery materials at adjustable angles, it adapts to diverse facility layouts. Ensures stable, spill-free transfer between floors or workstations. Ideal for warehouses, workshops, and construction sites. Boosts efficiency, simplifies material flow, and integrates seamlessly into production lines—reliable performance for streamlined operations. Core Functions 1. Material Conveying It can transport bulk materials (such as grain, snacks,dried fruits and meats, etc.) from low to high positions vertically or at a large inclination angle (usually >45°), addressing the height difference transportation needs that are difficult for traditional horizontal conveying equipment to meet. 2. Continuous and Efficient Operation Driven by a motor, chains or belts pull the buckets to move cyclically. The buckets sequentially complete loading, lifting, and unloading actions, enabling continuous material conveying and improving production efficiency. 3. Adaptability to Various Material Properties Different types of buckets (such as deep buckets and shallow buckets) and conveying speeds can be selected based on material characteristics like particle size, humidity, and specific gravity, ensuring stable conveying without material spillage. Main Features - Compact Structure: Small floor space, suitable for scenarios with limited space. - Easy Operation: Stable in operation with low maintenance costs, and can realize automatic start-stop through control systems. With its efficient and flexible characteristics, the bucket elevator has become an important equipment for vertical material conveying in industrial production.
MORE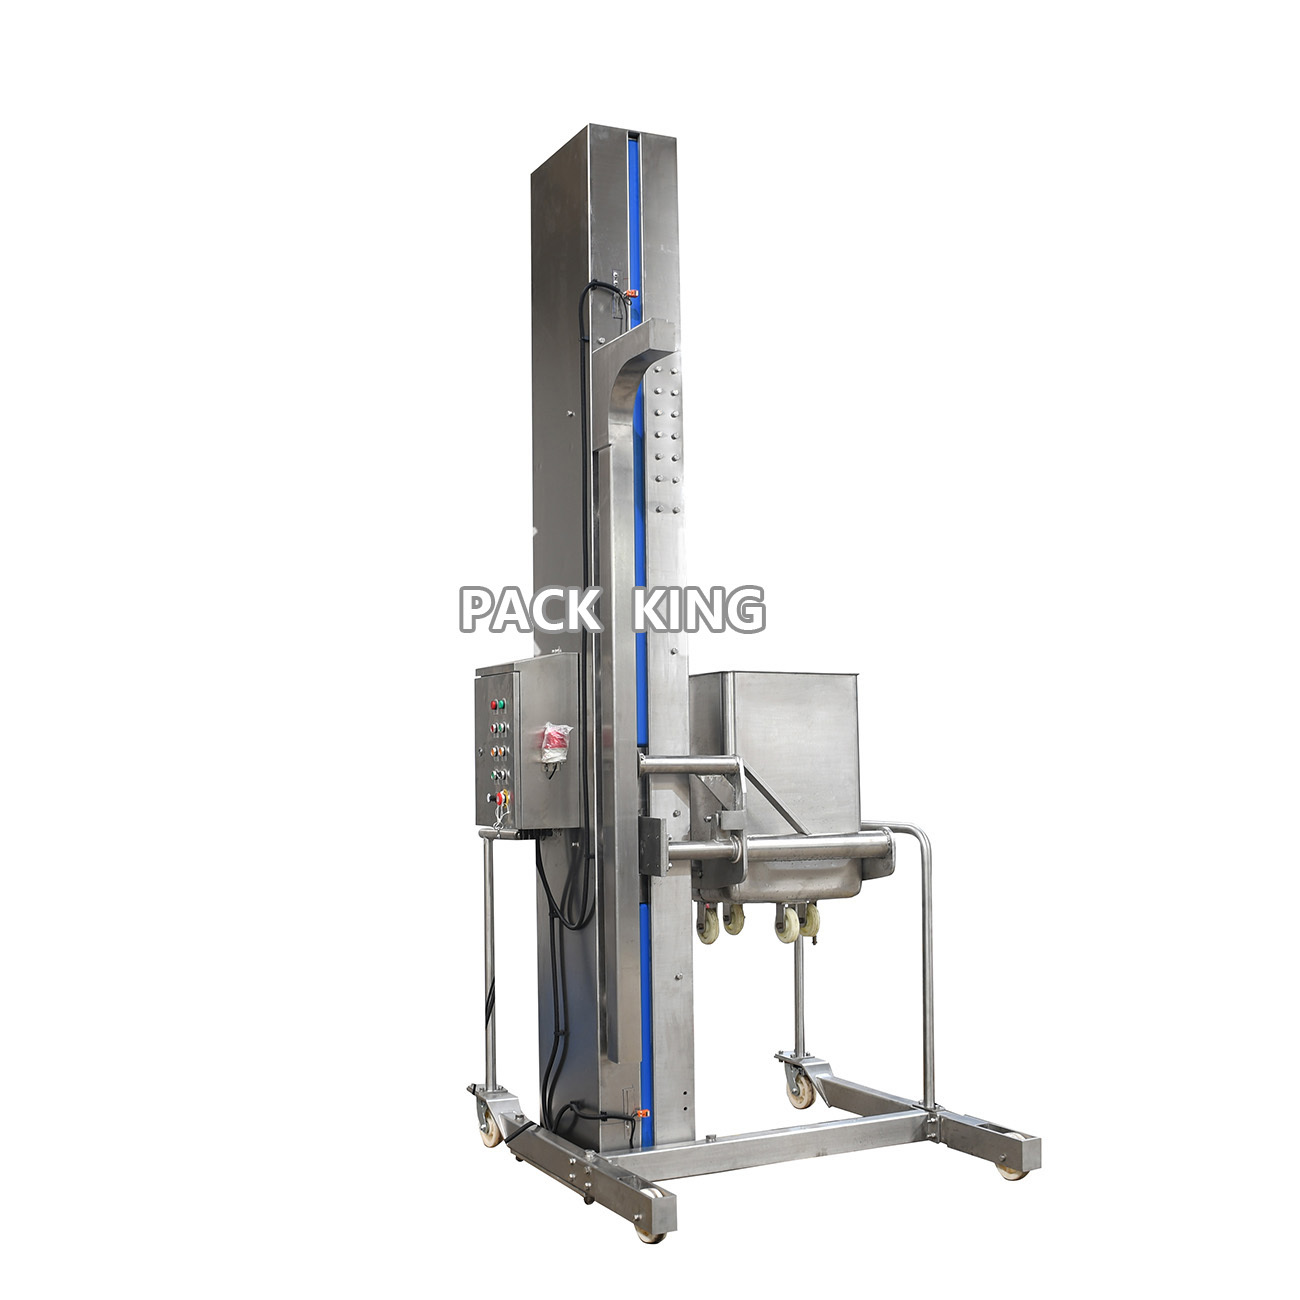
Vertical single-bucket elevator with trolley function: A versatile solution merging vertical bulk material lifting with flexible trolley transport. Ideal for workshops, warehouses, and construction sites. Effortlessly lifts granular/powdery materials vertically, then uses the integrated trolley for smooth horizontal transfer. Saves space, boosts efficiency, and simplifies material flow. A must-have for streamlined logistics in manufacturing and distribution sectors.
MORE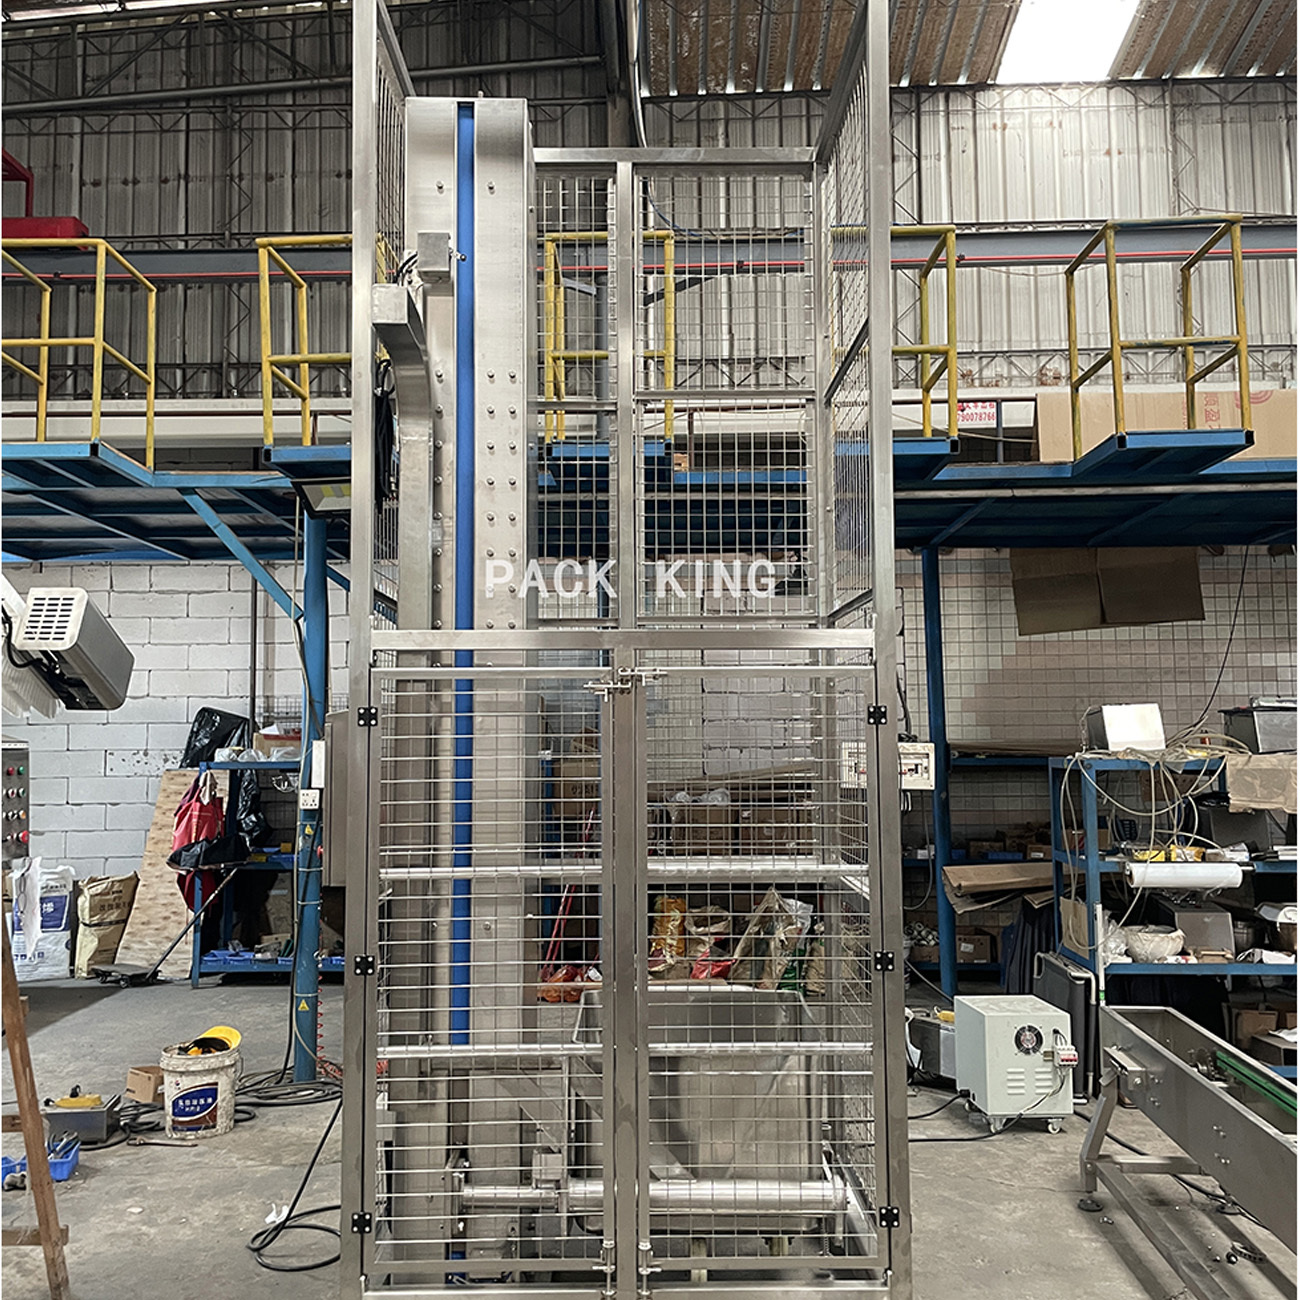
Vertical single bucket elevator with cage design
Vertical single-bucket elevator with safety door: A secure solution for bulk material lifting. The integrated safety door prevents accidents, blocks debris, and ensures operator protection during vertical transfer. Ideal for workshops, warehouses, and manufacturing floors. Maintains smooth material flow while enhancing workplace safety. Boosts compliance, reduces risks, and streamlines operations. Perfect for industries prioritizing safety without compromising efficiency—essential for secure production workflows.
MORE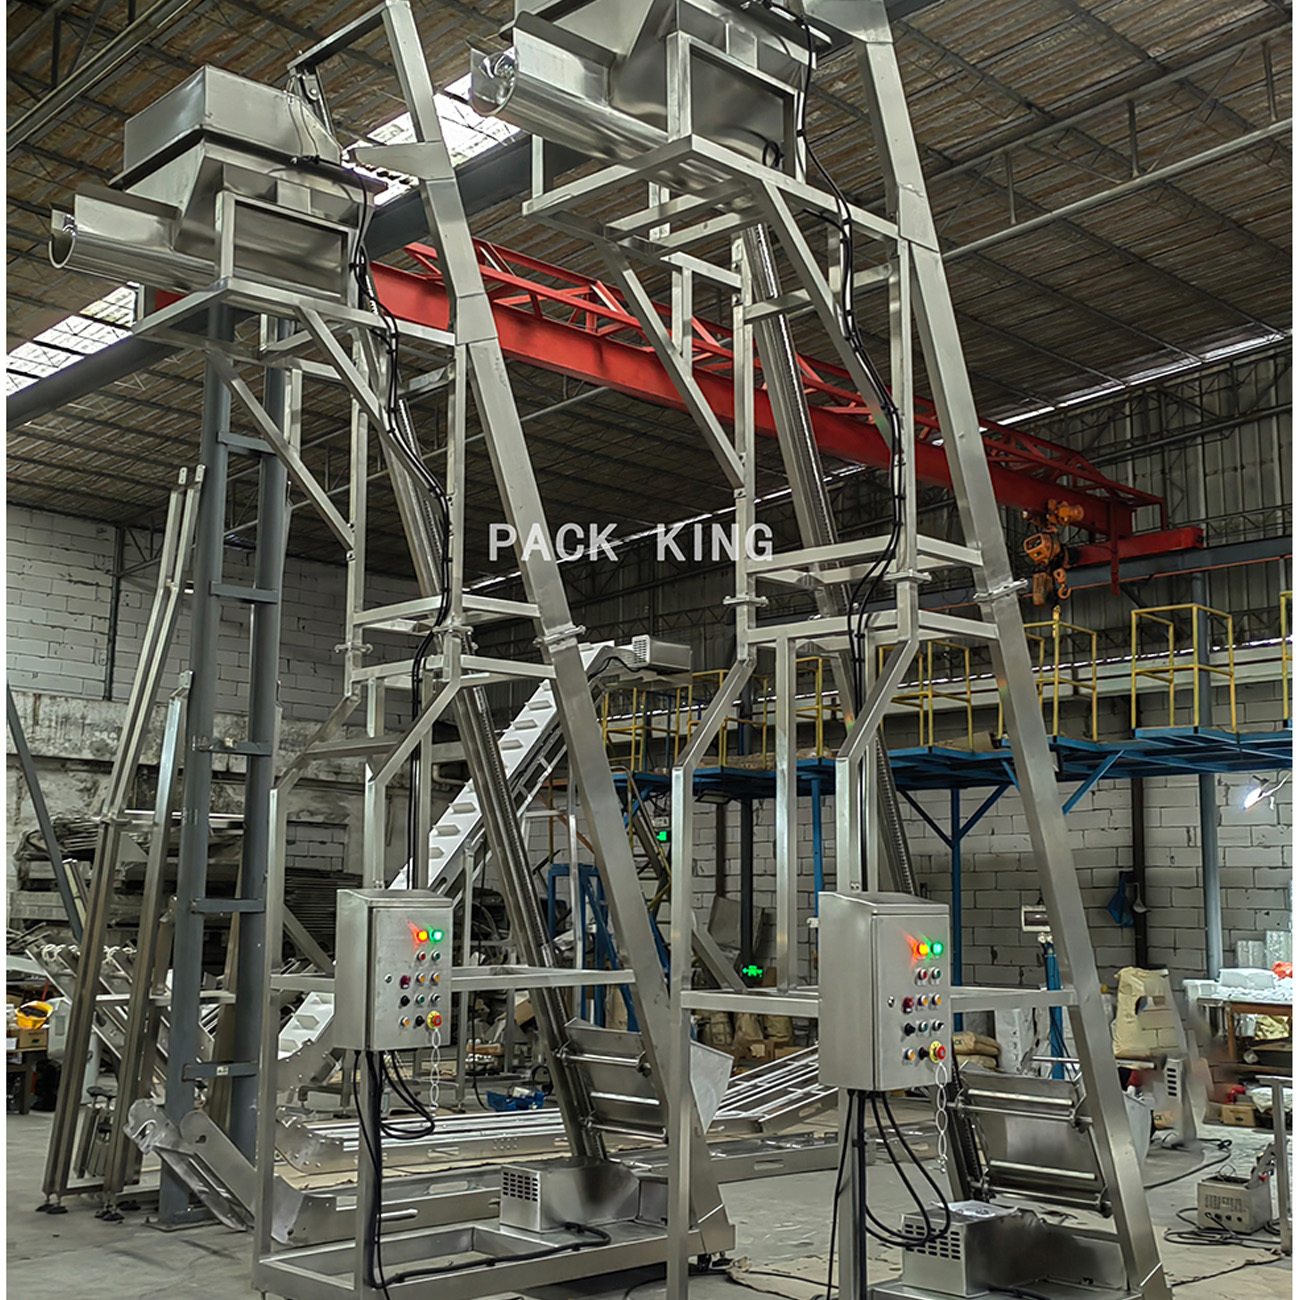
Inclined single bucket elevator combines screw feeder
Inclined single-bucket elevator paired with screw feeder: A powerful combo for bulk material handling. The screw feeder delivers precise, controlled material flow, while the inclined elevator lifts with stability. Prevents spillage, ensures uniform feeding, and adapts to varied layouts. Ideal for agriculture and manufacturing. Boosts efficiency, reduces waste, and streamlines production lines—essential for seamless material transfer.
MORE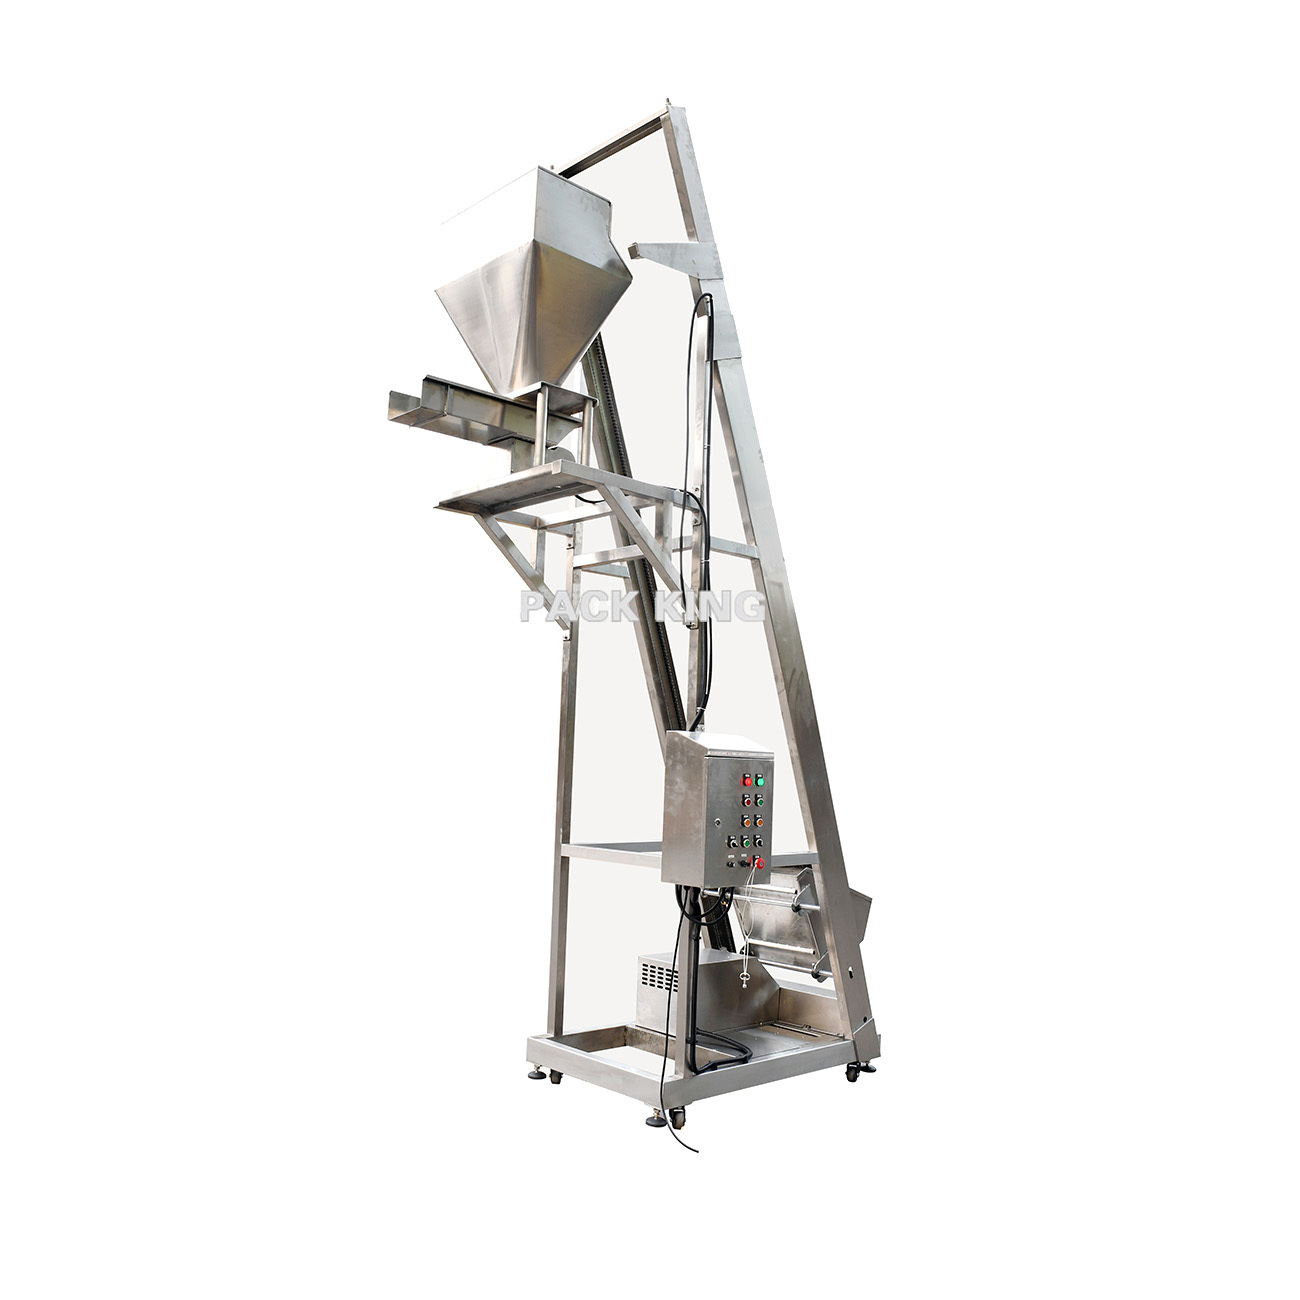
Inclined single bucket elevator combines vibrating feeder
Inclined single-bucket elevator with vibratory feeder: A high-performance combo for bulk handling. The vibratory feeder delivers steady, controlled material flow, while the inclined elevator lifts at adjustable angles with precision. Prevents clogging, reduces spillage, and adapts to facility layouts. Ideal for mining, agriculture, and manufacturing. Boosts efficiency, ensures safety, and streamlines production—essential for seamless material workflows.
MORE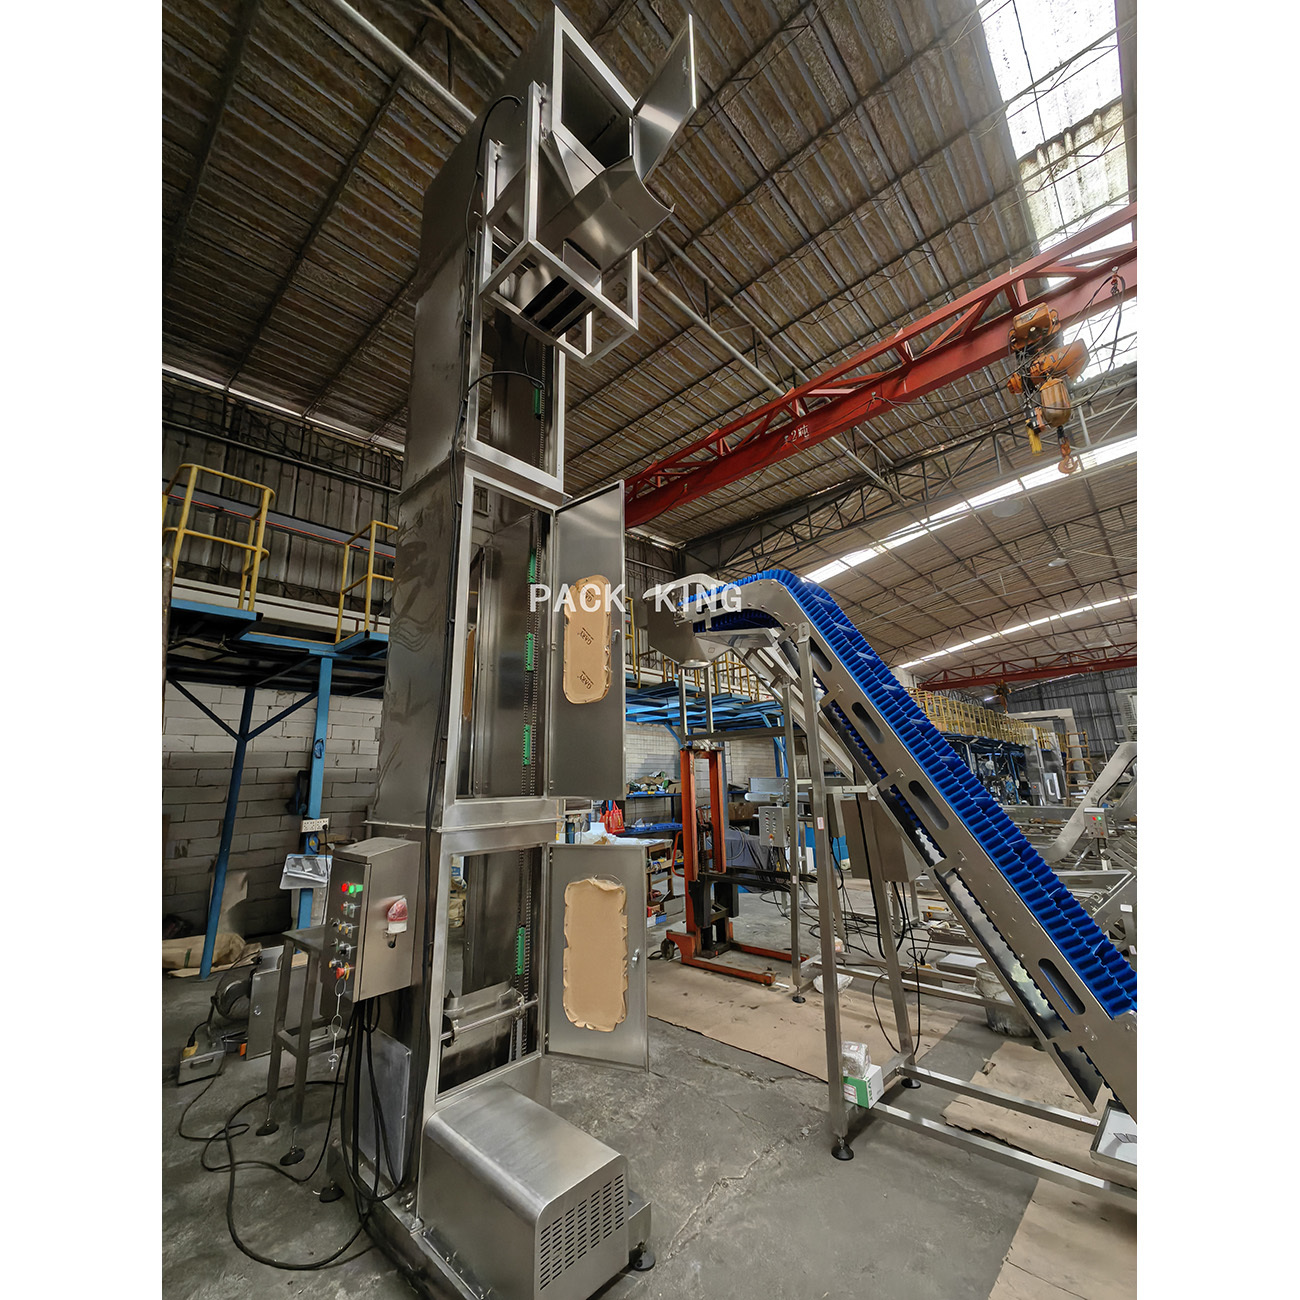
Vertical single bucket elevator combines vibrating feeder
Vertical single-bucket elevator with vibratory feeder: A dynamic duo for bulk material handling. The vibratory feeder delivers uniform, controlled material flow, while the elevator lifts vertically with precision. Prevents clogging, ensures consistent feeding, and streamlines workflows. Ideal for mining, agriculture, and manufacturing. Boosts efficiency, reduces downtime, and optimizes material transfer. A must-have for seamless, high-performance production lines.
MORE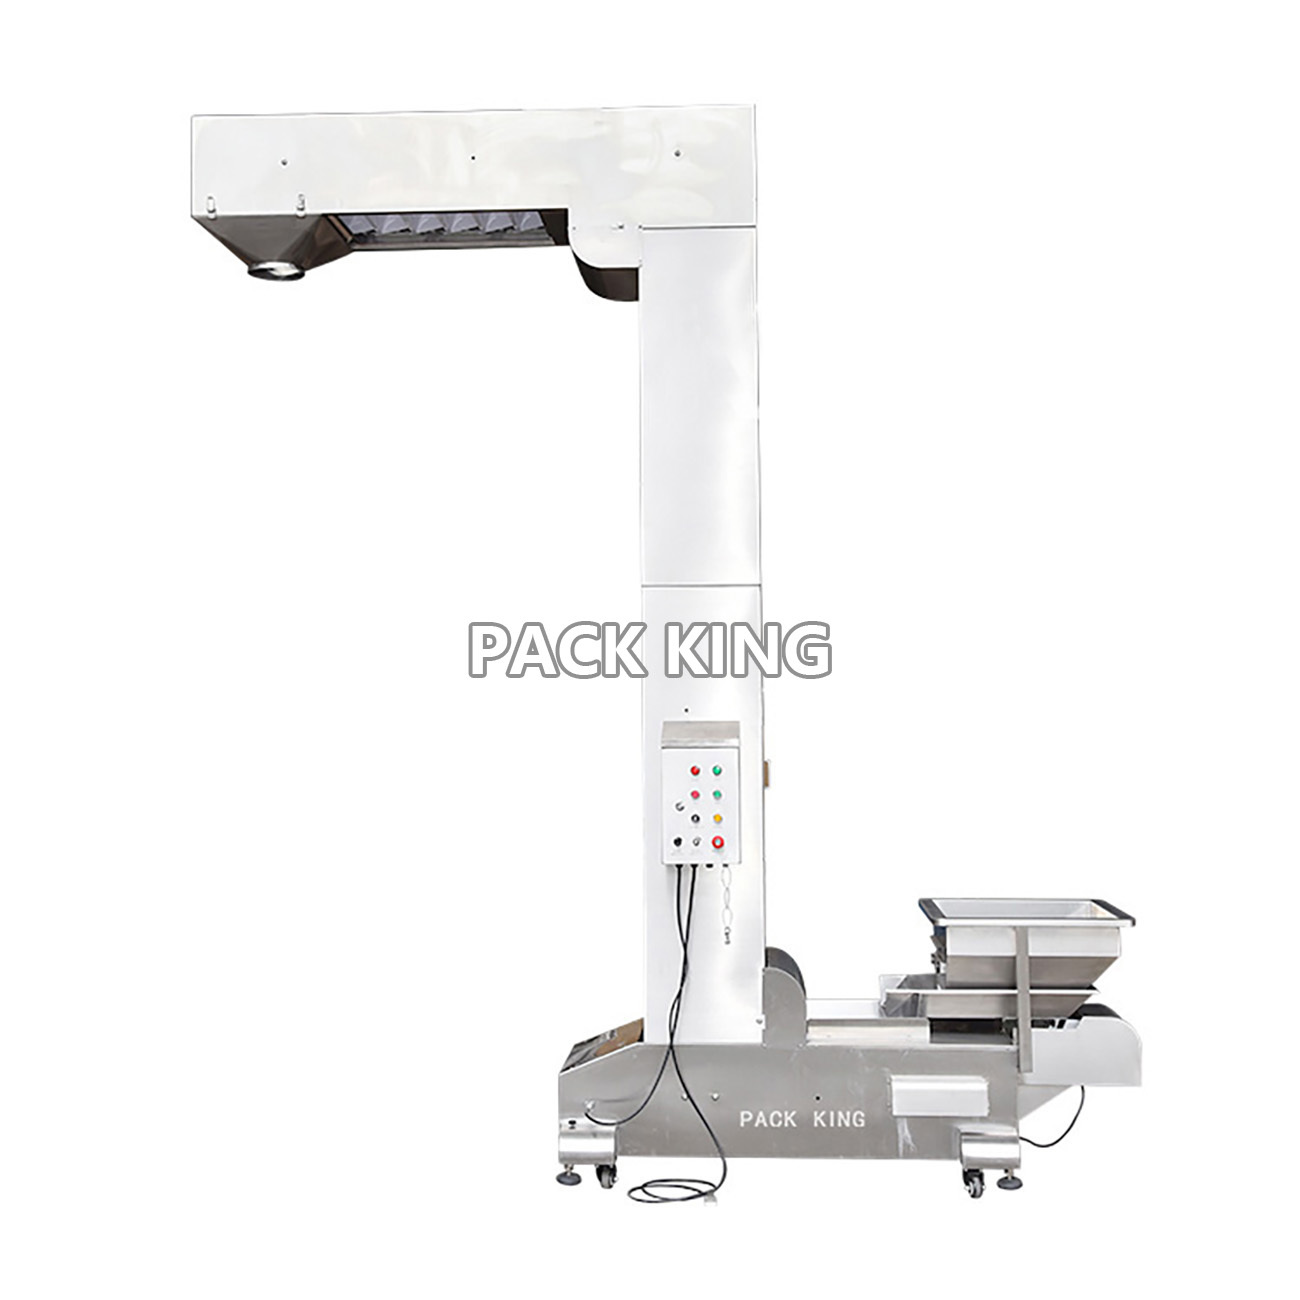
PP bucket elevator The Z-type elevator transports materials by continuously moving buckets attached to a chain Z-shaped path. The buckets are loaded at the bottom horizontal section, elevated vertically, and then discharged at the top horizontal section by tipping or tilting, enabling efficient, enclosed conveyance of powdered and granular materials between multiple floors. Mainly used for conveying good fluidity of food, crops, such as: peanuts, soybeans, rice, candy, dried fruit and other food, but also used for hardware, chemical, pharmaceutical, granular material transportation. Z- bucket elevators allow feeding control in one or more positions and can be easily inter-operated with various types of feeding devices. All components have easy removal inspection covers and easy positioning inspection Windows. The bucket has a quick release mechanism for quick installation or removal of the bucket. All elevators are equipped with automatic zippers and built- in overload protection.
MORE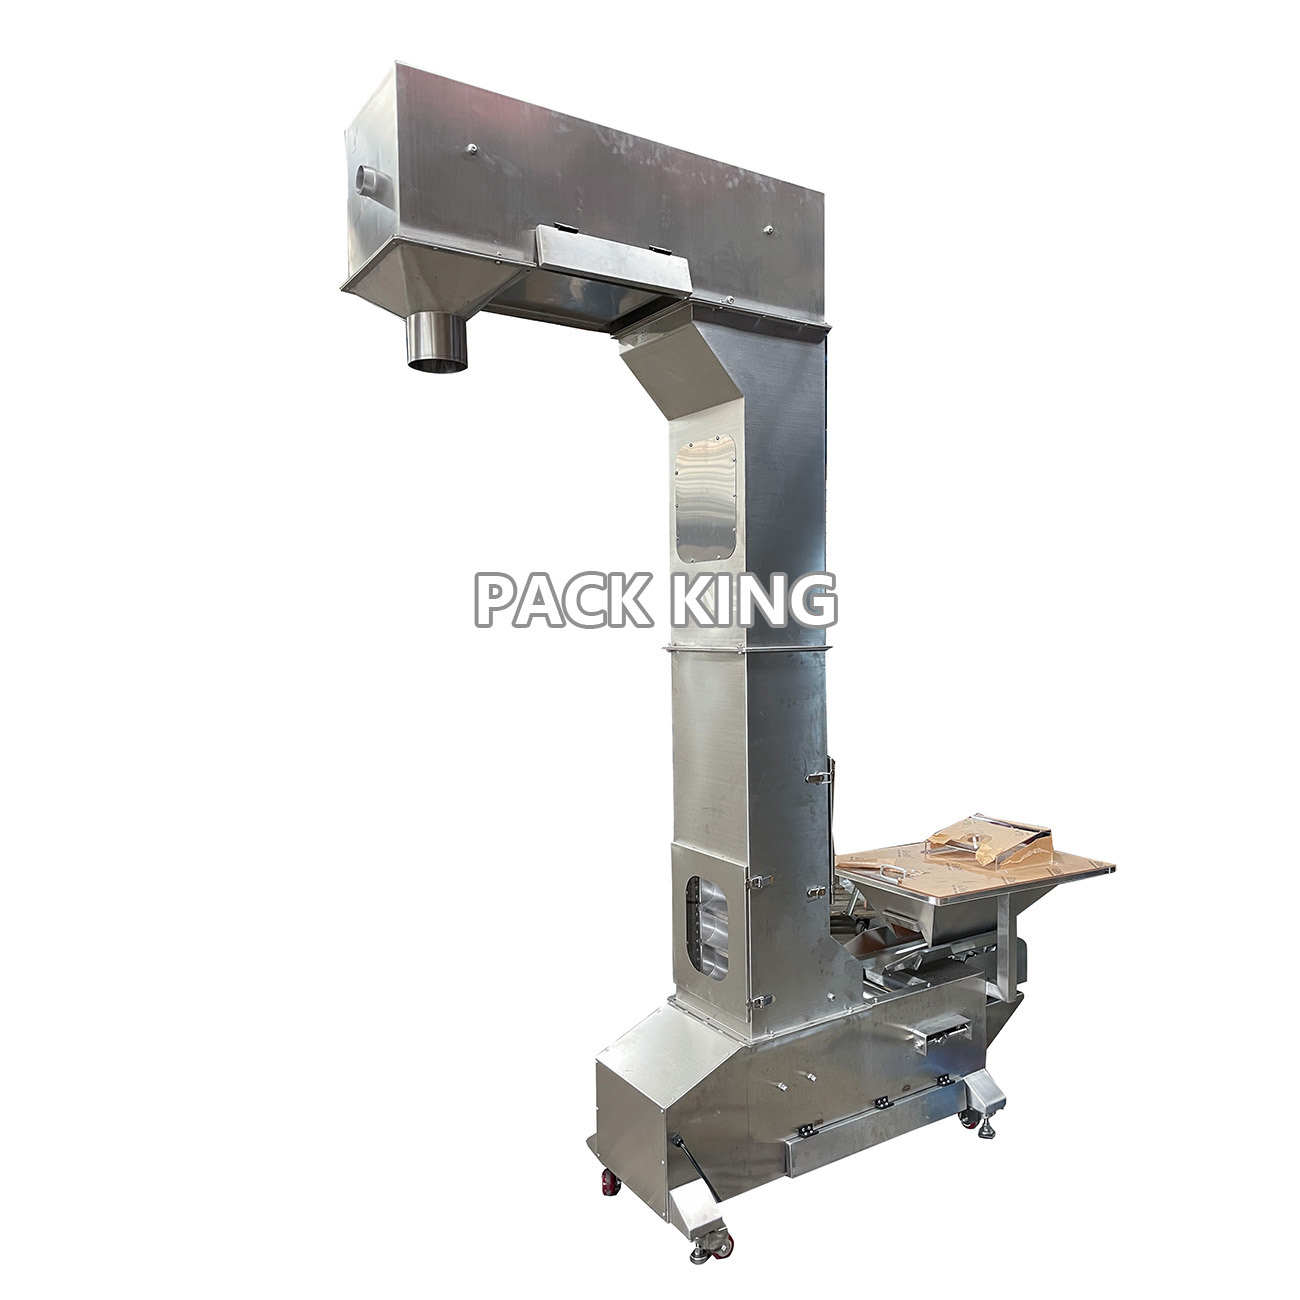
304 stainless steel bucket elevator
304 stainless steel bucket elevator When the buckets are made of stainless steel, the Z-type elevator is particularly suitable for applications in industries such as food processing, pharmaceuticals, and chemicals that demand strict hygiene, corrosion resistance, or high-temperature tolerance. It is ideal for conveying moist materials, oily granules, detergent ingredients, or solid materials requiring high-temperature sterilization, ensuring long-term durability and compliance with industry hygiene standards.
MOREQuick Quote
* Note: Please be sure to fill in the information accurately and keep the communication open. We will get in touch with you as soon as possible

Mobile/WhatsApp
Address
Building 4, Yinghao Intelligent Manufacturing Park, No.9 Xiashi Avenue, Xiashi Village, Lunjiao Subdistrict, Shunde District, Foshan City, Guangdong Province, China
Follow Us